How to Modernize a Potato Cold Storage in India: An Engineering Audit Sequence
Expert perspective: Alexander Samsonov, Agricultural Storage Engineer. Read the original LinkedIn perspective.
An old potato cold store is rarely improved by replacing one compressor or adding a larger fan. The first task is to understand how the building, crop, airflow, refrigeration and daily operating decisions interact.
This article develops an engineering sequence described by Alexander Samsonov: begin with the product and air path, then decide which equipment actually needs to change.
1. Establish the Storage Objective
Table potatoes, seed potatoes and processing potatoes do not have the same quality targets. Before measuring equipment, define the variety, expected loading period, storage duration, dispatch pattern, acceptable weight loss and the buyer's temperature, fry-colour or sprouting requirements.
The audit should also record incoming tuber temperature, soil load, mechanical damage, maturity and the time available for wound healing. A cold store cannot correct poor intake quality; it can only manage the crop that enters it.
2. Map the Building Envelope and Heat Loads
In a hot climate, the roof, end walls, doors, service openings and unsealed joints can add a major thermal load. Inspect insulation continuity, vapour control, solar exposure, door traffic and condensation marks before increasing refrigeration capacity.
- Use thermal imaging and surface-temperature measurements to identify heat bridges.
- Check whether warm humid air enters through doors, hatches or cable penetrations.
- Review drainage and surfaces where condensate can reach potatoes or packaging.
- Separate transmission, infiltration, product, fan and lighting loads in the cooling calculation.
3. Measure the Air Path, Not Only the Fan Nameplate
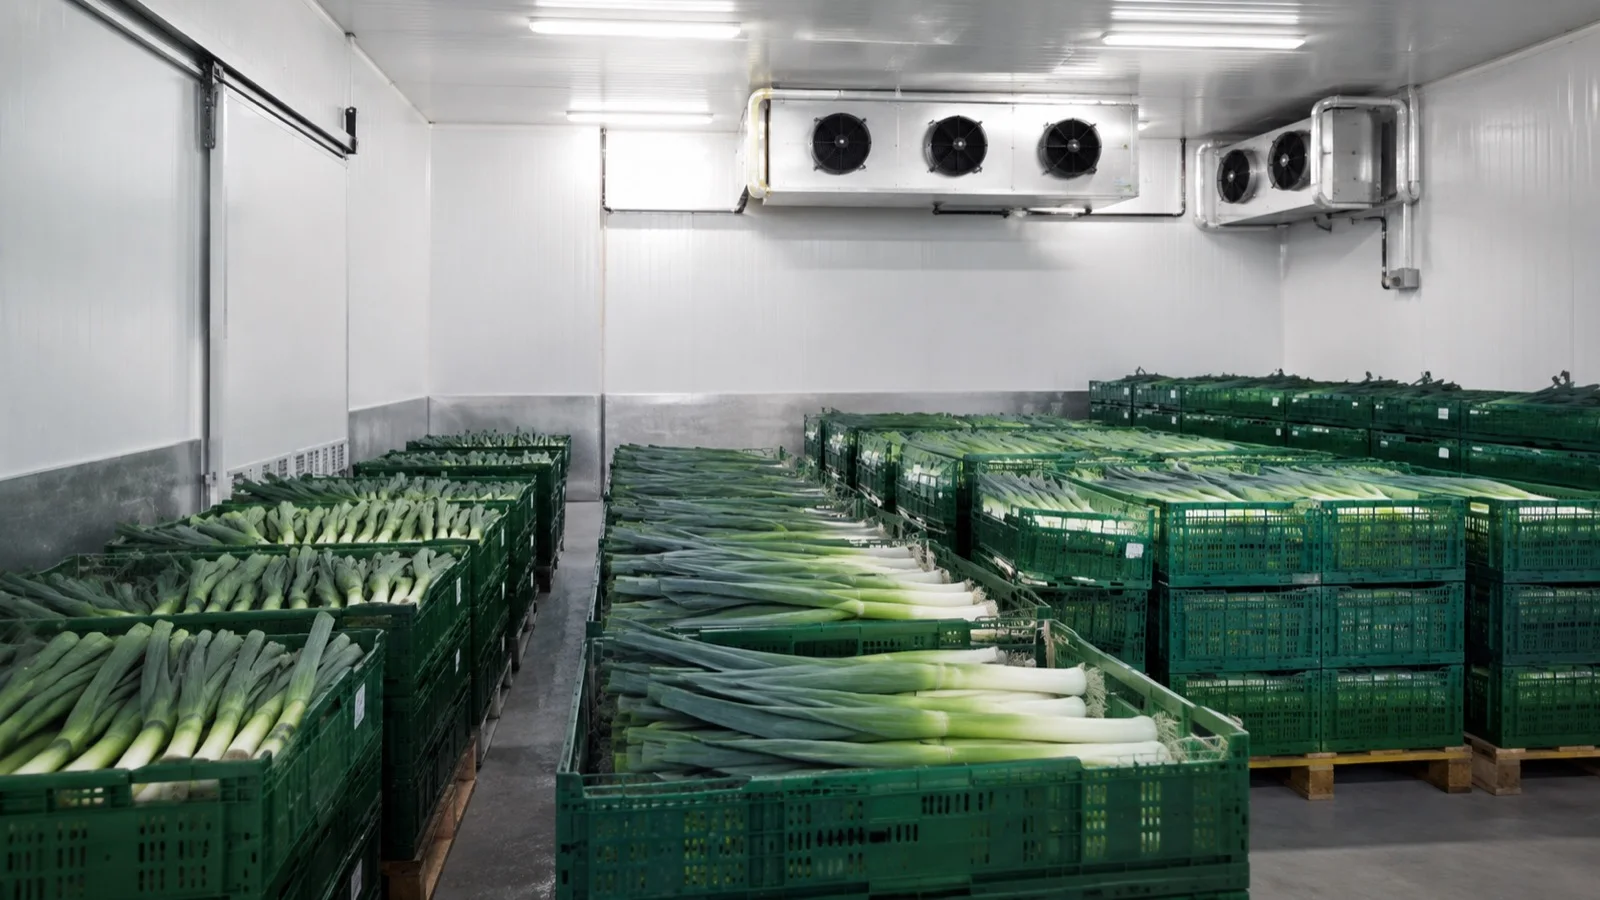
Walk the entire circuit: return air, mixing chamber, fan inlet, pressure plenum, ducts or floor openings, product load and exhaust path. Record static pressure and airflow at representative points. Smoke testing, pressure measurements and temperature mapping can expose short circuits and stagnant areas that are invisible on the controller screen.
Uniformity is the goal. A high average airflow does not help if the easiest route receives too much air while distant bags, bins or bulk zones remain warm.
4. Correct Ventilation Before Oversizing Cooling
Ventilation removes respiration heat and helps equalise temperature, moisture and gas concentration. Refrigeration removes heat from the system, but it cannot compensate for an air-distribution network that fails to bring warm product air back to the evaporator.
Depending on the existing structure, modernization may require redesigned plenums, controlled fresh-air and exhaust dampers, corrected fan placement, better sealing, local recirculation or a new distribution system. Fan selection must be based on airflow at calculated static pressure.
5. Add Cooling as a Controlled Stabiliser
After the envelope and airflow are understood, recalculate refrigeration for the real operating scenario. Coil design, temperature difference, defrost strategy, condensate drainage and fan heat all influence crop dehydration and room stability.
Cooling schedules must follow variety and market requirements. Processing potatoes, for example, may require a warmer holding strategy than other potato classes to manage reducing sugars and fry colour. Set points copied from another facility are not a commissioning plan.
6. Make the Control Logic Understandable
A modernization is incomplete if the operator cannot explain why a fan, damper, cooler or humidification stage is running. The control screen should show measured crop and air conditions, operating mode, equipment state, alarms and trends that support a decision.
- Separate curing, pull-down, holding, ventilation and dispatch modes.
- Use representative sensors and validate their placement after loading.
- Trend temperature spread, humidity, CO₂ and equipment runtime.
- Document manual overrides and the conditions for returning to automatic control.
7. Validate the Result Under Load
Commissioning an empty room proves only that equipment starts. A useful acceptance test is performed with real product and records temperature uniformity, airflow, pressure, energy use, dehydration and product quality over a defined period.
The modernization sequence is: product objective → envelope → air path → ventilation → refrigeration → automation → operating procedure. Reversing that order often purchases capacity without solving the loss mechanism.
Review Agrovent's vegetable storage engineering and existing-building reconstruction guide. For an initial audit discussion, send the facility capacity, location and current storage method to Agrovent India.
Sources and Further Reading


More articles
 Smart Farming: How Big Data impact Agriculture
It is expected that the use of Big Data will have a great impact on agriculture and cover the entire supply chain, will change the roles and attitudes of market players.
News
 Why Onion Drying Determines Storage Success: Best Practices for Tropical & Temperate Climates
Proper onion drying is the most critical step before storage. Learn why inadequate drying leads to bacterial rot, neck rot, and 20–80% storage losses, and discover the best drying methods for temperate and tropical climates.
Harvest
 Why Do Potato Sprouts Sometimes Grow Inward During Storage?
Inward potato sprouting occurs from storage stress - not genetics. Stable temperature, humidity, and ventilation prevent damage and preserve quality.
News
 How to reduce your food waste
Almost 1.3 billion tons of food produced per year is lost or discarded. How does this affect us and the environment?
News
 What is permaculture?
Basic principles and history of permaculture
News
 HRMN-99: The Heat-Tolerant Apple Variety Transforming Farming in India’s Plains
Discover how HRMN-99, a self-pollinating, heat-tolerant apple variety developed in Himachal Pradesh, is enabling farmers across India’s tropical and subtropical regions to grow apples successfully—even at 40–45°C.

Leave your contacts and we will get back to you